Most bulk material blockages in mining don’t need more force. They need a better diagnosis before anyone spends money on flow aids. A planned assessment establishes what is happening in the hopper, whether compressed air fits, and what safety and compliance work has to happen first.
Clarify what the blockage looks like from safe records
The first job is describing the failure in plain terms so an engineer can work with it later, before picking hardware.
In mining hoppers, silos, bins, and chutes, poor flow usually follows a few patterns. A rathole leaves a narrow central channel while dead material packs against the walls. A bridge forms a stable arch over the outlet and stops flow all at once. Side-wall buildup narrows the flow path over time and makes discharge slow and uneven. Those patterns point to different causes, and they don’t respond to the same fix.
The assessment should draw on existing records. Stoppage logs, control room trends, level readings, discharge rates, and photos from approved observation points give a better picture than memory. Note whether the problem starts when the level drops low, after rain, after a change in ore source, or after extended storage. Record what clears it today and how long that takes. That history matters.
Don’t try to confirm the blockage up close. Don’t approach the outlet, lean over a hatch, poke at hung material, or enter the bin to look. Stored material can release without warning, and air above it can hold dust and low oxygen. Engulfment and stored pressure are real hazards, along with dust exposure and unexpected remote firing once flow aids are installed. All inspection and clearing steps must follow the site’s authorized site procedure.
Bring in qualified bulk-flow review early
Once the pattern is clear on paper, get a qualified bulk-flow engineer involved before choosing equipment. This is a technical review of material, vessel shape, and operating limits, rather than a sales visit.
The engineer will want material facts, not guesses. Moisture content, cohesion, particle size, temperature, and wall adhesion all change how material hangs up. Abrasiveness and heat matter too, since they affect liner wear and what type of intervention will last. Operating context counts as much as lab results. Hopper angle, outlet size, storage height, feed rate, and drawdown practice determine where stress builds in the stored mass.
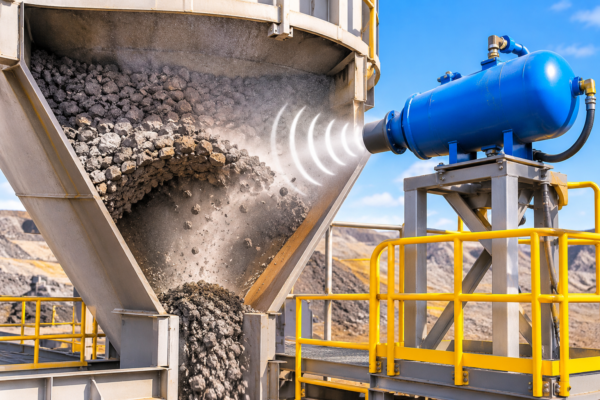
That review should also compare options. An air cannon is one flow aid among several in mining service. Mechanical vibrators, bin-whip systems, chute changes, moisture control, and changes to fill and draw practice can be better answers. There is no automatic best choice across all arches and ratholes. The engineer judges whether a timed air pulse fits the material and vessel, or whether another method will last longer with less upkeep.
Keep the site team involved. Operations knows when the plant pushes throughput, while maintenance knows what fails and safety knows where people get exposed today. That input grounds the assessment in how the hopper actually runs.
Audit air and site services through specialists
If the engineer sees a possible fit for compressed air, the next check is services. This step is often skipped, and many installations fall short here.
Air cannons need a strong burst of air at the right moment. That takes more than a large compressor elsewhere in the plant. Line size, line length, leaks, receiver volume, and demand from other users all affect what arrives at the hopper. Dust and heat add load to filters, solenoids, and controls. Power for timers and sensors has to be stable, and cable runs need protection.
Have a compressed-air specialist assess capacity at the planned location, not just at the compressor room. The review should cover available flow and pressure under normal plant load, receiver placement, moisture in the air lines, and filtration needs. It should also flag noise and dust around discharge points, since a blast can stir fines.
Don’t use generic capacity rules from handbooks or past jobs. Use the supplier’s actual model data for the units under review, checked against site measurements. A mining ring main that looks ample on a drawing can still drop off at a distant hopper when drills, workshops, and baghouses draw at once. There’s no shortcut here. If the air isn’t there, the cannon won’t work no matter how well it is mounted.
Specify tank, valve and nozzle approach as an engineering decision
Equipment selection follows material and services review. That order keeps the project from buying tanks first and making excuses later.
Tank size, valve layout, nozzle count, and mounting position all interact. A larger tank holds more blast energy, but it also adds weight, air use, and reaction load. Valve placement affects exposure to heat, dust, and abrasive fines, plus access to seals and solenoids for service. Nozzle aim decides whether the pulse hits the obstruction zone or just packs material tighter against the far wall. Small shifts in position can change the result.
Once the assessment establishes that an air cannon is the right flow aid, the specification moves to valve type, tank size, placement, and controls; the equipment itself is only one part of the plan.
Treat external-valve and internal-valve layouts as trade-offs to discuss with the engineer and supplier, not as fixed answers for fixed materials. Access for service, contact with sticky or abrasive product, operating temperature, and mount geometry all pull in different directions. The right choice depends on that mix, plus what maintenance crews can reach safely on day and night shifts.
The same care applies to mounts and nozzles. Hopper walls vary in thickness and stiffness. Liners, stiffeners, and existing cracks change what can be cut and welded. The engineer should define positions on a drawing tied to the obstruction zone identified in the records, with access left clear for inspection. Fabrication and installation then follow site welding and cutting controls.
Design controls and interlocks for people, not just flow
Controls decide whether the system helps or creates new exposure. In mining plants, cannons often sit above conveyors, feeders, and walkways where people work. The control design has to protect those areas first.
A normal setup uses timers or a PLC with level inputs and firing outputs. Sequenced firing can prevent units from discharging together. Sensors can hold firing when the bin is empty or downstream equipment is stopped. Those functions need clear documentation so operators know what the system will do next.
Interlocks are not optional extras. Firing must be blocked when access doors are open, when guards are removed, during maintenance on the bin or feeder, and when people are assigned under the vessel. Lockout and tagout points must isolate both electrical control power and stored air in tanks and lines. Remote firing from the control room needs clear warning and local isolation, since unexpected discharge can drop lumps and throw dust.
Keep test and service modes under the same authorized procedure. There should be no informal way to fire a unit by hand near the hopper. Training should cover what a misfire looks like and how to confirm zero stored pressure, along with who can return the system to auto. That discipline matters more than timer settings.
Address structure, pressure vessel status and maintenance access together
Structure, compliance, and service access belong in one assessment. They all affect where a cannon can sit and what it will cost to own.
Start with the vessel. A hopper or chute wall that already flexes, cracks liners, or spills at joints won’t improve with added load. A structural engineer should confirm that walls, stiffeners, and support steel can take static weight plus blast reaction. Mount brackets need proper design and installation control, with weld checks to site standard. If reinforcement is needed, price it into the plan.
Pressure vessel status comes next. Air cannon tanks are pressurized air receivers, which brings inspection and record duties. AS/NZS 3788 provides the benchmark for the in-service inspection scheme, with the scheme documented before the equipment connects to the mine compressed-air system. Records should show vessel identity, inspection dates, findings, and repairs. Procurement should address design registration and paperwork with the supplier so the site isn’t chasing documents after installation.
Then walk the service path. Can a fitter reach valves, solenoids, filters, and drains without a scaffold build every time? Check for light, safe footing, and isolation within sight. Remote mining sites can’t afford long shutdowns for simple seal swaps. Noise near blast points, dust from discharge, and heat near dryers or hot product also shape access times and PPE. Good placement shortens those jobs and keeps them routine. Poor placement turns each callout into a permit-heavy event that crews put off, and delays don’t help flow.
Build the business case and pilot with agreed acceptance measures
A sound plan ends with numbers the plant trusts. Pull a baseline for the prior quarter from existing site records. Stoppage hours tied to the hopper, manual clearing labor, spill cleanup, conveyor overloads, and wear-liner damage tell the cost story. Safety exposure tells the rest. Count confined-space entries and work at height near the bin, as well as clearing with bars or lances under load.
Use that baseline to set acceptance measures with operations, maintenance, and safety. Measures might cover fewer unplanned stops on that hopper, no need for entry clearing, less spillage at the feeder, and stable drawdown at target rate. Tie them to plant records so results aren’t argued later. Budget for installation, air and power upgrades, controls work, structural changes, inspection setup, spares, and service time, not just the cannon price.
Run a staged pilot on one high-impact hopper under an authorized plan. Install to the engineered drawing, commission with the interlocks proved, then track the same baseline measures through normal mining variation, including wet periods and source changes. Review with the team that set the targets. If the pilot meets the agreed measures and service load stays workable, plan wider rollout unit by unit. If it doesn’t, the data will show whether the cause is air supply, placement, material change, or the wrong method.
A careful assessment won’t promise easy flow. It will show where compressed air helps, what it takes to run it safely, and what it costs over time. That answer holds up with crews, engineers, and managers alike.